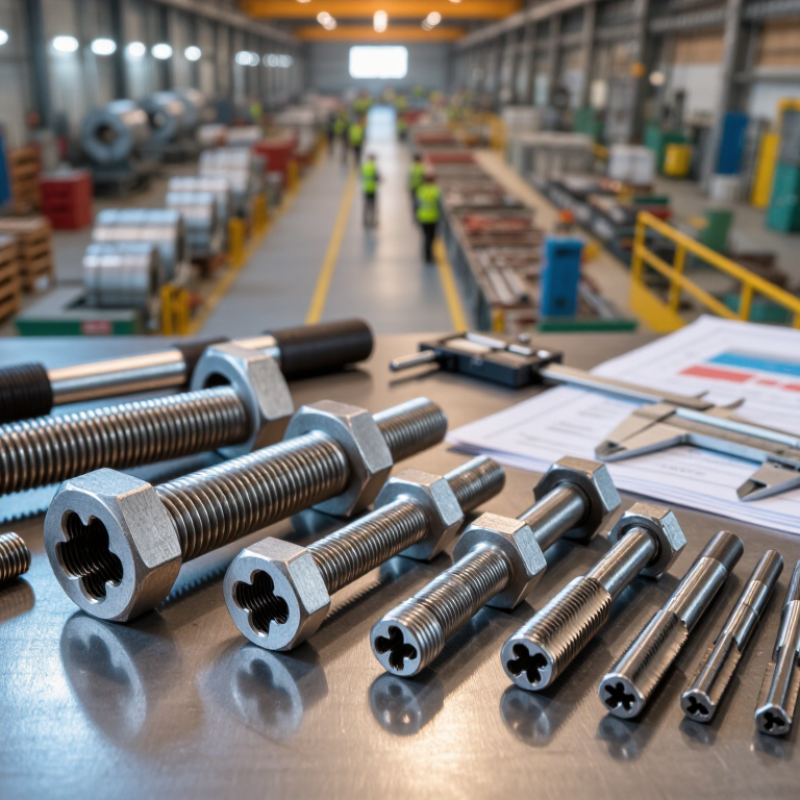
| Product Definition | Double-end bolts, commonly called double-ended studs, have external threads on both ends and an unthreaded or partially threaded center section. | Confirm the screwed-end length, nut-end length, overall length, thread pitch, thread class, and center-body diameter on the approved drawing. | Technical drawing, dimensional specification, and signed order confirmation. |
| Common Dimensional Standards | DIN 938 is commonly used for studs with a short screwed end; DIN 939 is commonly used for studs with a longer screwed end. | Ensure the selected standard matches the equipment design and that metric dimensions are not mixed with inch dimensions. | Applicable standard designation, revision date, and customer-approved product drawing. |
| Mechanical Property Classes | ISO 898-1 defines mechanical and physical properties for carbon-steel and alloy-steel bolts, screws, and studs. Common property classes include 8.8, 10.9, and 12.9. | Check tensile strength, yield or proof strength, hardness, and the required property class for the application. | Mill test certificate, mechanical test report, and batch traceability record. |
| High-Temperature or Pressure Applications | ASTM A193 covers alloy-steel and stainless-steel bolting for high-temperature or high-pressure service. Grade B7 is a widely specified alloy-steel grade under this standard. | Confirm the required material grade, heat-treatment condition, temperature range, and compatibility with the mating components. | Material certificate, heat-treatment record, chemical analysis, and mechanical test results. |
| Material Traceability | Traceability normally links each production batch to a heat number, raw-material certificate, production record, and final inspection report. | Verify that the marking and documentation identify the same batch shipped in the container or package. | Heat-number records, batch labels, inspection reports, and packing-list references. |
| Thread Accuracy | Metric external threads are commonly specified with ISO metric thread profiles, while inch threads may use Unified National Coarse or Unified National Fine profiles. | Confirm nominal diameter, pitch or threads per inch, tolerance class, thread direction, and effective thread length. | Thread plug and ring gauge records, dimensional inspection report, and sample approval. |
| Coating and Corrosion Protection | ISO 4042 addresses electroplated coatings for fasteners, while ISO 10683 addresses non-electrolytically applied zinc-flake coatings. | Specify coating type, coating thickness, corrosion requirement, hydrogen-embrittlement controls, and torque-tension requirements where applicable. | Coating certificate, thickness report, salt-spray test report when contractually required, and process-control record. |
| Quality Management | ISO 9001 is an internationally recognized quality-management-system standard. Certification applies to the documented management system and stated scope. | Check the certificate validity, certification scope, issuing certification body, and whether the manufacturing site is covered. | Current ISO 9001 certificate and certification-body verification record. |
| Inspection and Acceptance | ISO 3269 provides general requirements for acceptance inspection of fasteners unless a purchase contract specifies different requirements. | Define sampling level, critical dimensions, visual requirements, mechanical tests, nonconformance handling, and inspection responsibility before production. | Inspection and test plan, first-article report, final inspection report, and agreed acceptance criteria. |
| Export Classification | Iron or steel threaded bolts and similar fasteners are generally classified under HS heading 7318.15, subject to the exact product description and customs rules. | Confirm the tariff subheading with the customs broker in the destination country because national tariff extensions may differ. | Commercial invoice, product description, HS code confirmation, and customs declaration data. |
| Export Documentation | Typical international shipments use a commercial invoice, packing list, transport document, and, where applicable, a certificate of origin. | Make sure quantities, net and gross weights, package marks, part numbers, Incoterms® rule, and consignee information are consistent across documents. | Commercial invoice, packing list, bill of lading or air waybill, certificate of origin, and insurance document when required. |
| Packaging for Overseas Transport | Fasteners are commonly packed in sealed inner bags or cartons, placed in export-suitable cartons, and secured on pallets or in crates where needed. | Specify corrosion-inhibiting packaging, moisture protection, package weight limits, carton markings, pallet requirements, and container loading instructions. | Approved packaging specification, packing photographs, package-weight record, and loading checklist. |
| Pre-Shipment Inspection | Inspection may include quantity verification, visual examination, dimensions, thread gauging, hardness, tensile testing, coating checks, and document review. | Agree whether inspection is performed by the manufacturer, an independent inspection agency, or the buyer’s representative. | Pre-shipment inspection report, test certificates, photographs, and nonconformance closure record. |
| Delivery Planning | Actual production and transport time depends on size, material, coating, quantity, tooling, inspection requirements, port schedules, and destination country. | Request a written production schedule with drawing approval, raw-material arrival, machining, heat treatment, coating, inspection, packing, and dispatch milestones. | Manufacturing schedule, order milestone report, booking confirmation, and shipping advice. |
| After-Sales Support | Professional support normally covers technical clarification, replacement of verified nonconforming goods, corrective-action analysis, and document reissue. | Define response time, claim-submission period, evidence requirements, replacement or credit procedure, freight responsibility, and warranty exclusions. | Written warranty terms, claims procedure, corrective-action report, and approved replacement policy. |
| Supplier Selection Indicator | A reliable manufacturer should be able to provide consistent specifications, traceable batches, controlled inspection records, export documentation, and clear contractual responsibilities. | Evaluate technical capability, quality-system evidence, sample consistency, communication speed, delivery performance, and transparency of nonconformance handling. | Supplier questionnaire, sample inspection, audit report, reference project evidence without confidential customer information, and signed quality agreement. |